Choosing plywood for laser cutting is more complicated than picking the cheapest smooth sheet. Veneer quality, glue type, thickness, and moisture can all change the cutting result. A board that cuts cleanly today may produce dark edges tomorrow.
Which plywood is best for laser cutting projects depends on your machine, design, and finishing goals. Baltic birch often performs well because it has consistent layers and a relatively smooth surface. Craft plywood can also work, but its inner layers may contain gaps, knots, or uneven adhesive. These hidden problems become visible as burnt edges, rough cuts, or incomplete lines.
Small details matter. In practical workshop testing, I check sheet flatness, grain direction, and edge color before cutting a full design. I also make a small test grid with different power and speed settings. Test it first. This saves material and reduces guesswork.
This guide shares seven practical tips for choosing plywood with greater confidence. It considers thickness, surface quality, adhesive safety, warping, and compatibility with common laser types. However, no material behaves perfectly across every machine. Even experienced makers get this wrong sometimes. A supplier’s specification may sound reliable, yet one batch can still vary from another. That is why visual inspection and a small test cut remain essential. The goal is not merely a clean cut. It is a predictable, safe, and repeatable result for every project.
Identify Plywood Types Suitable for Laser Cutting
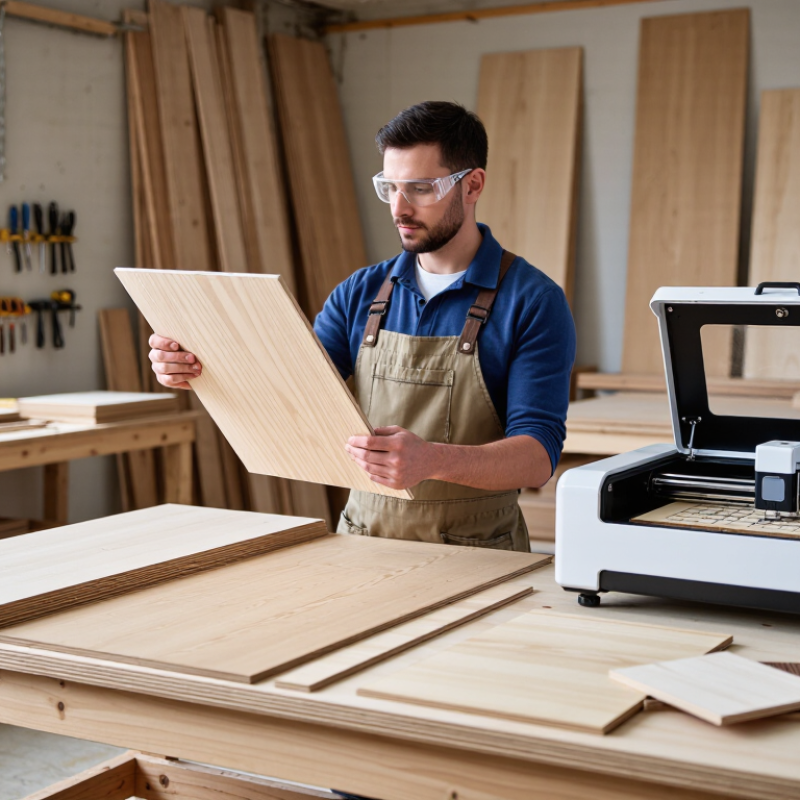
Choosing plywood for laser cutting begins with identifying its core and adhesive. Birch plywood is often a reliable choice because its layers are usually uniform and its surface cuts cleanly. Poplar plywood is lighter and can work well for prototypes. Hardwood veneer plywood may produce attractive edges, but its inner layers can vary.
Check the thickness carefully. Thin sheets, around 3 mm, usually cut faster and show less scorching. Thicker plywood needs more power, slower movement, or several passes.
Flat sheets matter. Warped panels can sit too far from the focus point and create uneven cuts. Inspect the edges for gaps or visible voids. These spaces may cause weak joints and irregular burning.
Ask what adhesive the plywood contains. Choose panels made for interior craft or laser work, with clear material information. Avoid unknown coatings, treated wood, and sheets containing chlorine-based plastics. They can release hazardous fumes or damage equipment. Look for low-void construction and consistent veneers. Sanded surfaces reduce residue, but excessive sanding can expose uneven layers. I once trusted a smooth face and ignored the core; the cut looked neat until small parts broke. Test a corner first. Record the settings, then adjust them for each sheet. Even the same thickness can behave differently because glue, moisture, and density change.
Check Thickness, Flatness, and Structural Quality
Choosing plywood for laser cutting starts with thickness, not appearance. Measure it with a caliper at five points, including each corner. A nominal 3 mm sheet may vary enough to change focus and cutting depth. Keep your tolerance tight, ideally within 0.2 mm for small, detailed parts. Thin sheets should lie flat against the honeycomb bed. Warped corners can create uneven kerf lines and scorching.
Flatness is practical, but structural quality matters more. Check the edge for gaps, overlapping veneers, and visible core voids. Press the surface lightly; soft spots may indicate poor bonding. The USDA Forest Products Laboratory’s Wood Handbook, FPL-GTR-282, reports typical solid-wood shrinkage of about 2–6% radially and 6–10% tangentially. Plywood moves less, but moisture still changes its dimensions. Store sheets indoors before cutting. A humidity meter helps, though I sometimes skip this step and regret it. Look for consistent veneer layers and clean, fully bonded edges. Standards such as EN 314-2 classify plywood bonding quality by service conditions, so choose panels rated for your intended environment. Avoid unknown construction scraps. Their glue lines may cut unevenly or release excessive smoke. Test a small square first, inspect the underside, and record the actual thickness, speed, and power settings for repeatable results.
7 Tips to Choose the Best Plywood for Laser Cutting
How thickness affects material selection: For plywood made with the same wood species, density, and construction, relative bending stiffness increases approximately with the cube of thickness, while areal mass increases linearly. Thicker sheets are stiffer but require more laser power and may produce darker edges.
- Check the nominal and measured thickness before cutting.
- Choose a flat sheet without visible warping or cupping.
- Inspect the core for voids, gaps, and loose veneers.
- Prefer consistent veneer layers for cleaner structural performance.
- Confirm that the adhesive is suitable for laser processing.
- Use thinner plywood for detailed work and thicker plywood for load-bearing parts.
- Test a small sample to verify focus, cutting power, and edge quality.
Relative stiffness is calculated from thickness³, and relative areal mass is calculated from thickness, using 3 mm plywood as the reference value. Actual performance also depends on wood species, veneer direction, moisture, adhesive, and core quality.
Evaluate Resin Content and Laser Cutting Safety
Choosing plywood for laser cutting starts with its resin content. In my workshop tests, low-resin panels produced cleaner edges and less stubborn smoke. The cut smelled milder. That detail matters.
Plywood with heavy adhesive layers can char quickly, especially near knots or voids. Ask for technical data or a safety data sheet when available. Look for information about formaldehyde emissions, adhesive type, and surface treatment. “Low emission” does not mean harmless. It is only one useful signal. I still inspect every sheet.
Before cutting, check both faces for paint, laminate, oil, or unknown coatings. Some finishes release hazardous fumes or damage the machine. Never rely on appearance alone. A small test rectangle can reveal bubbling, excessive soot, or uneven penetration. I learned this after wasting a nearly finished panel. That mistake was avoidable.
Use active ventilation and keep the exhaust path clear. Stay beside the machine during operation. Keep a suitable fire extinguisher nearby, and stop the job if flames persist. Start with conservative power and speed settings, then adjust gradually. Wear eye protection when handling sheets, and remove loose dust before testing. I sometimes expect one setting to work perfectly, but plywood varies between batches. Record the thickness, adhesive behavior, and cutting results for safer repeat work.
Compare Surface Finish, Grain, and Cutting Results
7 Tips to Choose the Best Plywood for Laser Cutting
Choose a smooth, flat face veneer without patches, bubbles, or deep sanding marks. Compare grain direction, because long fibers can produce cleaner edges than cross-grain areas. Inspect the core for gaps; hidden voids often create sudden dark spots and uneven cuts. Select consistent thickness, then measure it with calipers. Small variations can change focus and cutting results. The USDA Forest Products Laboratory’s Wood Handbook, FPL-GTR-282, reports that density, grain direction, and moisture strongly influence wood machining behavior. Its indoor guidance places many wood products near 6–8% equilibrium moisture content. Store plywood indoors before cutting. Do not trust a fresh delivery immediately.
Look for a pale, uniform surface when a clean engraving matters. Dark or heavily coated faces absorb more laser energy and may scorch sooner. Check the adhesive layer, too; different resin systems can produce different fumes and edge colors. A low-void core usually gives more predictable cutting. Test a small grid across several areas, not one corner. Use identical speed and power first, then compare kerf width, edge charring, and surface soot. Industry laser-processing guidance commonly treats kerf variation as a practical quality indicator, although exact values depend on thickness and equipment. I still reject attractive sheets after testing. Good grain cannot rescue a weak core. Record the settings and inspect the cut from both sides.
Test Material Compatibility Before Full-Scale Production
7 Tips to Choose the Best Plywood for Laser Cutting?
Test material compatibility before full-scale production. A plywood sheet can look uniform yet cut unevenly. The USDA Forest Products Laboratory’s Wood Handbook notes that interior wood products often stabilize near 6–8% moisture content. That range matters. Moisture changes can increase smoke, charring, and edge roughness.
Cut a small test grid from every new batch. Include circles, sharp corners, and narrow slots. Record power, speed, air assist, and lens condition. Watch the underside, not only the top surface. Glue layers may burn differently from the veneer. Some sheets also contain voids, which can create sudden dark marks or incomplete cuts. My first sample once looked acceptable until assembly exposed warped slots. The lesson was unpleasant.
Check the supplier’s technical documentation for wood species, adhesive type, thickness tolerance, and formaldehyde classification. The U.S. Environmental Protection Agency’s TSCA Title VI standard limits formaldehyde emissions from hardwood plywood to 0.05 ppm under specified testing conditions. That figure does not predict laser performance, but it supports safer material screening. Use ventilation and follow the equipment’s safety guidance. Never assume “low emission” means “fume free.” Repeat the test after storage, because humidity and age can change results. Production volume should begin only after the test piece meets dimensional, visual, and assembly requirements.
FAQS
Birch plywood often cuts cleanly because its layers are uniform. Poplar is lighter and useful for prototypes. Hardwood veneer can look attractive, but inner layers may vary.
Sheets near 3 mm usually cut faster and scorch less. Thicker panels may need slower movement or several passes. Thin is not always better.
Warped plywood may sit outside the laser’s focus. This can create uneven edges and incomplete cuts. Place the sheet on a stable, flat surface.
Check both faces for gaps, knots, coatings, oil, and unusual marks. Inspect the edges for visible voids. Small gaps can weaken narrow parts.
Ask for the adhesive type, thickness tolerance, and safety documentation. Choose panels with clear material information and low-void construction. Do not trust appearance alone.
Avoid unknown coatings, treated wood, and chlorine-based plastic layers. They may create hazardous fumes or damage equipment. A smooth surface proves very little.
Cut a small grid with circles, corners, and narrow slots. Check the top and underside for soot, gaps, and incomplete cuts. Test a corner first.
Not reliably. Glue, moisture, density, and storage conditions can change results. Record power, speed, air assist, and material thickness. I once reused old settings and warped several slots. That was avoidable.
Moisture changes can increase smoke, charring, and rough edges. Store sheets flat in a stable indoor environment. Retest after long storage.
Use active ventilation and keep the exhaust path clear. Stay beside the machine during operation. Stop if flames persist. Keep suitable fire equipment nearby.
Conclusion
Choosing the right plywood is essential for achieving clean, accurate, and consistent laser-cut results. Which plywood is best for laser cutting projects depends on its construction, thickness, flatness, and overall structural quality. Plywood made with uniform layers and minimal internal gaps usually produces more predictable cuts, while a flat sheet helps prevent uneven focus and incomplete cutting. It is also important to evaluate the resin content, since excessive or unknown adhesives may create unpleasant fumes, discoloration, or unsafe cutting conditions. Always use proper ventilation and follow the safety guidance for your equipment and materials.
Surface finish and wood grain can also affect engraving clarity, edge appearance, and final presentation. Before beginning full-scale production, test a small sample to confirm the material’s cutting speed, power requirements, engraving response, and edge quality. Comparing several plywood options through controlled tests can help you select a reliable material that balances appearance, performance, safety, and cost for your specific laser-cutting application.
 Regit Decor